Chemical plant equipment forms the physical and mechanical foundation of facilities that manufacture, process, separate, store, and transfer chemical substances. These facilities use combinations of reactors, pumps, heat exchangers, vessels, columns, filtration systems, compressors, storage tanks, instrumentation, and automated control systems.
The configuration of chemical plant equipment depends on the process chemistry, operating temperature and pressure, material characteristics, production scale, safety requirements, and environmental controls. Modern manufacturing systems increasingly combine mechanical equipment with process automation, digital monitoring, and advanced instrumentation.
Context
What Is Chemical Plant Equipment?
Chemical plant equipment refers to machinery and engineered systems used throughout chemical processing facilities. Individual components perform specific functions, while interconnected equipment creates a complete process flow.
A chemical plant may contain equipment for reaction, heating, cooling, mixing, separation, filtration, drying, compression, storage, and material transfer.
Major Categories of Chemical Plant Equipment
Chemical processing equipment can generally be grouped according to its primary function.
| Equipment Category | Main Function | Typical Applications |
|---|---|---|
| Process Reactors | Chemical reactions | Synthesis and polymer processing |
| Heat Exchangers | Heat transfer | Heating and cooling |
| Distillation Columns | Component separation | Solvent and chemical separation |
| Storage Tanks | Material storage | Raw materials and intermediates |
| Pumps | Liquid transfer | Process circulation |
| Compressors | Gas compression | Process gas systems |
| Filters | Solid-liquid or gas separation | Purification and clarification |
| Dryers | Moisture removal | Powders and chemical products |
| Mixers | Material blending | Chemical formulation |
| Pressure Vessels | Controlled containment | High-pressure processes |
The equipment combination varies significantly between different chemical manufacturing processes.
Process Reactors
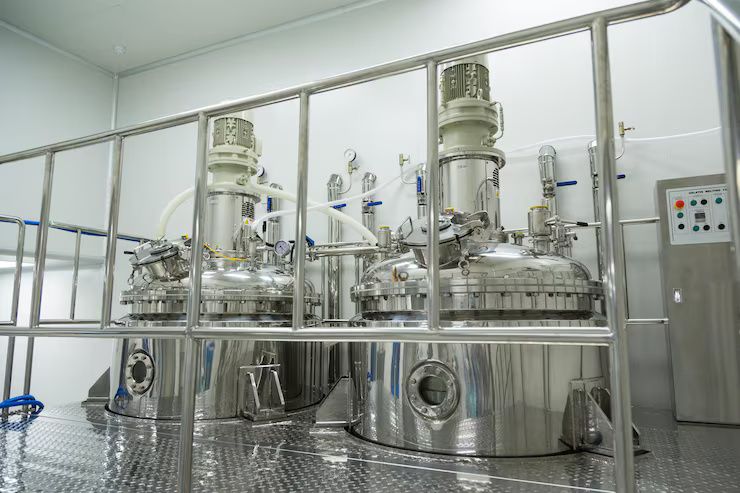
Reactors provide controlled environments for chemical reactions. Their design can include agitation systems, heating or cooling jackets, internal coils, pressure-control components, and instrumentation.
Reactor materials are selected according to chemical compatibility, temperature, pressure, corrosion characteristics, and cleaning requirements.
Heat Exchangers
Heat exchangers transfer thermal energy between process streams. They are commonly used to heat raw materials, cool reaction mixtures, condense vapors, or recover thermal energy.
Common configurations include shell-and-tube, plate, air-cooled, and specialized heat-exchange systems.
Distillation Equipment
Distillation systems separate components according to differences in volatility. A typical system may include a column, reboiler, condenser, reflux system, trays or packing, and process instrumentation.
Distillation is used across chemical, petrochemical, pharmaceutical, food-processing, and related industries.
Pumps and Compressors
Pumps move liquids through process piping, while compressors increase the pressure of gases.
Equipment selection depends on factors such as flow rate, pressure differential, fluid properties, temperature, viscosity, and chemical compatibility.
Importance
Why Chemical Plant Equipment Matters
Chemical processes often operate under controlled temperature, pressure, flow, and composition conditions. Equipment must therefore maintain process conditions while containing potentially reactive, corrosive, flammable, or hazardous materials.
Proper equipment selection and system design can contribute to process stability, operational reliability, worker protection, and environmental control.
Supporting Process Manufacturing
Chemical plants commonly use multiple process stages. Raw materials may pass through reactors, separators, heat exchangers, filters, dryers, storage vessels, and other equipment before reaching the final processing stage.
The equipment must work as an integrated system rather than as isolated components.
Material Selection
Materials of construction are important in chemical plant equipment. Stainless steels, carbon steels, alloys, polymers, glass-lined materials, and other specialized materials may be selected depending on the process environment.
Factors can include corrosion resistance, mechanical strength, temperature range, pressure conditions, and compatibility with process chemicals.
Process Control
Instrumentation and automation provide continuous information about equipment and process conditions.
Sensors can measure:
- Temperature
- Pressure
- Flow
- Level
- pH
- Composition
- Vibration
- Equipment status
These measurements can be transmitted to PLC, DCS, SCADA, or other control platforms.
Equipment Reliability
Chemical plants may operate continuously or for extended production campaigns. Equipment reliability is therefore an important engineering consideration.
Maintenance programs can include inspection, calibration, lubrication, vibration monitoring, pressure testing, and planned component replacement according to equipment requirements.
Manufacturing Systems and Process Technologies
Batch Processing
Batch chemical manufacturing processes produce a defined quantity of material during each production cycle. Reactors, mixers, vessels, and transfer systems can be configured around individual batches.
Batch processing is commonly associated with specialty chemicals, pharmaceuticals, coatings, formulations, and other products requiring flexible production arrangements.
Continuous Processing
Continuous chemical processes maintain a steady flow of raw materials through interconnected equipment.
Continuous systems can include reactors, heat exchangers, separation columns, pumps, compressors, and control loops operating together over extended periods.
Separation Technologies
Separation is an important part of many chemical processes. Technologies can include:
- Distillation
- Filtration
- Centrifugation
- Membrane separation
- Absorption
- Adsorption
- Crystallization
- Evaporation
The appropriate technology depends on the physical and chemical properties of the materials involved.
Mixing Systems
Industrial mixers combine liquids, solids, gases, or combinations of these materials. Impeller design, vessel geometry, mixing speed, viscosity, and residence time all influence system performance.
Mixing equipment can be installed inside reactors, storage tanks, formulation vessels, and dedicated blending systems.
Drying Technologies
Industrial dryers remove moisture or other volatile components from chemical products. Common technologies include tray dryers, rotary dryers, fluidized-bed dryers, spray dryers, and vacuum dryers.
Selection depends on material properties, required moisture levels, thermal sensitivity, and production conditions.
Industrial Applications
Petrochemical Processing
Petrochemical facilities use extensive process equipment for separation, reaction, heat transfer, compression, storage, and material handling.
Distillation columns, reactors, compressors, pumps, heat exchangers, and storage systems are among the major equipment categories.
Specialty Chemicals
Specialty chemical plants often use batch reactors, mixers, filtration systems, dryers, storage vessels, and dosing equipment.
Process flexibility and accurate control can be important where multiple formulations or chemical processes are conducted within the same facility.
Pharmaceutical Manufacturing
Pharmaceutical plants use reactors, mixing systems, filtration equipment, dryers, purified-water systems, storage vessels, and other process equipment.
Equipment design may need to support cleaning, contamination control, material traceability, and applicable manufacturing requirements.
Fertilizer Production
Fertilizer manufacturing involves reaction, granulation, drying, cooling, screening, material transfer, and storage operations.
Large industrial systems can incorporate reactors, granulators, dryers, conveyors, fans, scrubbers, and material-handling equipment.
Water and Wastewater Treatment
Chemical treatment plants use pumps, dosing systems, mixers, tanks, filters, membranes, and separation equipment.
Automation systems can monitor water quality and regulate chemical dosing according to defined process conditions.
Food and Ingredient Processing
Chemical and biochemical processing equipment can also be used in food and ingredient manufacturing. Heat exchangers, mixers, reactors, evaporators, filtration systems, and dryers can support various processing stages.
Equipment selection must consider hygiene, material compatibility, temperature, and product characteristics.
Suppliers and Manufacturing Ecosystem
Chemical plant equipment suppliers can specialize in individual equipment categories or provide integrated process systems. Manufacturers may produce reactors, vessels, heat exchangers, pumps, filtration systems, separation equipment, or complete process modules.
When evaluating suppliers, organizations commonly examine:
- Equipment specifications
- Materials of construction
- Pressure and temperature ratings
- Capacity and throughput
- Instrumentation compatibility
- Automation integration
- Documentation
- Inspection requirements
- Maintenance accessibility
- Applicable standards
Engineering requirements should be established before equipment selection so that individual components remain compatible with the overall process design.
Recent Updates
Industrial Automation
Modern chemical plants increasingly use automated control architectures. PLCs and DCS platforms can regulate process variables while HMIs provide operators with process information.
Automation can coordinate pumps, valves, heaters, coolers, agitators, compressors, and other equipment.
Advanced Instrumentation
Newer instrumentation can provide more detailed information about equipment and process conditions.
Digital transmitters, smart sensors, online analyzers, and condition-monitoring devices can contribute to improved process visibility.
Industrial IoT
Connected equipment can transmit operating information to centralized data platforms. Industrial IoT architectures can support equipment monitoring, energy analysis, production tracking, and maintenance planning.
Network design and cybersecurity remain important considerations for connected industrial systems.
Predictive Equipment Monitoring
Vibration, temperature, pressure, electrical, and other measurements can be analyzed to identify changes in equipment behavior.
Predictive approaches can support maintenance planning by helping teams investigate potential issues before equipment performance is significantly affected.
Energy Management
Chemical processes can require substantial heating, cooling, compression, pumping, and separation. Energy-monitoring systems can track equipment consumption and identify process areas requiring further engineering analysis.
Heat recovery and process integration can also reduce unnecessary thermal losses.
Modular Process Equipment
Modular process systems can combine multiple components into prefabricated units. Depending on the application, modularization can simplify installation and support standardized equipment arrangements.
Skid-mounted reactors, filtration systems, dosing systems, and utility modules are examples of modular configurations.
Laws or Policies
Process Safety
Chemical plants require comprehensive process-safety programs because some processes involve hazardous materials, high temperatures, high pressures, or reactive substances.
Risk assessment, operating procedures, emergency planning, equipment inspection, and process-control measures form part of broader safety management.
Pressure Equipment Requirements
Pressure vessels, boilers, piping, and related equipment may be subject to specific engineering and inspection requirements.
Applicable codes and regulations depend on the equipment category, jurisdiction, operating conditions, and facility type.
Hazardous Area Requirements
Facilities handling flammable gases, vapors, or dust may require equipment designed for hazardous environments.
Electrical and instrumentation equipment should be selected according to the applicable area classification and certification requirements.
Environmental Regulations
Chemical plants may be subject to regulations covering emissions, wastewater, waste handling, chemical storage, and environmental monitoring.
Facility operators need to identify the specific requirements applicable to their process and location.
Occupational Safety
Worker safety programs can address chemical exposure, machinery hazards, confined spaces, pressure systems, personal protective equipment, emergency response, and other workplace risks.
Tools and Resources
Process Simulation Software
Process simulation tools can model flows, temperatures, pressures, material balances, energy balances, and equipment interactions.
Engineers can use these models during process development and equipment design.
Piping and Instrumentation Diagrams
P&IDs provide detailed representations of process equipment, piping, valves, instrumentation, and control loops.
They are important references during engineering, construction, commissioning, operation, and maintenance.
Computerized Maintenance Management Systems
CMMS platforms can track equipment records, inspections, preventive maintenance activities, calibration schedules, and maintenance history.
Digital Control Platforms
DCS, PLC, and SCADA systems provide process monitoring and control capabilities. These platforms can collect data from field instruments and coordinate automated equipment.
Equipment Inspection Tools
Inspection technologies can include ultrasonic testing, radiographic testing, magnetic particle testing, visual inspection, vibration analysis, and other nondestructive testing methods.
These techniques can help evaluate equipment condition without necessarily removing components from operation.
FAQs
What is chemical plant equipment?
Chemical plant equipment includes machinery and engineered systems used for chemical processing, reaction, separation, heating, cooling, mixing, filtration, storage, compression, and material transfer.
What equipment is commonly found in a chemical plant?
Common equipment includes reactors, heat exchangers, distillation columns, pumps, compressors, storage tanks, pressure vessels, filters, dryers, mixers, and process-control systems.
How is automation used in chemical plants?
Automation systems collect measurements from sensors and use controllers to regulate equipment such as pumps, valves, heaters, coolers, mixers, and compressors.
What factors influence chemical plant equipment selection?
Important factors include process chemistry, temperature, pressure, flow rate, material compatibility, capacity, corrosion conditions, safety requirements, maintenance needs, and applicable engineering standards.
Who manufactures chemical plant equipment?
The manufacturing ecosystem includes specialized producers of reactors, heat exchangers, pumps, compressors, vessels, filtration equipment, separation systems, automation equipment, and integrated process modules.
Conclusion
Chemical plant equipment provides the mechanical foundation for modern chemical processing. Reactors, heat exchangers, separation systems, pumps, compressors, storage vessels, filtration equipment, dryers, and automation systems work together to transform raw materials through controlled industrial processes.
Advances in industrial automation, smart instrumentation, Industrial IoT, predictive monitoring, modular equipment, and energy management are changing how chemical plants are designed and operated. Equipment selection should remain closely connected to process chemistry, materials engineering, safety requirements, environmental considerations, maintenance strategies, and applicable regulations.